KUD02200-050VJ15-900-000 slewing bearing 1962.8×2376mm
News & Updates
KUD02200-050VJ15-900-000 slewing bearing 1962.8×2376mm
Dimensional Envelope and Load Capacity Interpretation
At a glance
- Specification Parameter: Value
- Model Number: KUD02200-050VJ15-900-000
- Inner Diameter: 1962.8 mm
- Outer Diameter: 2376 mm
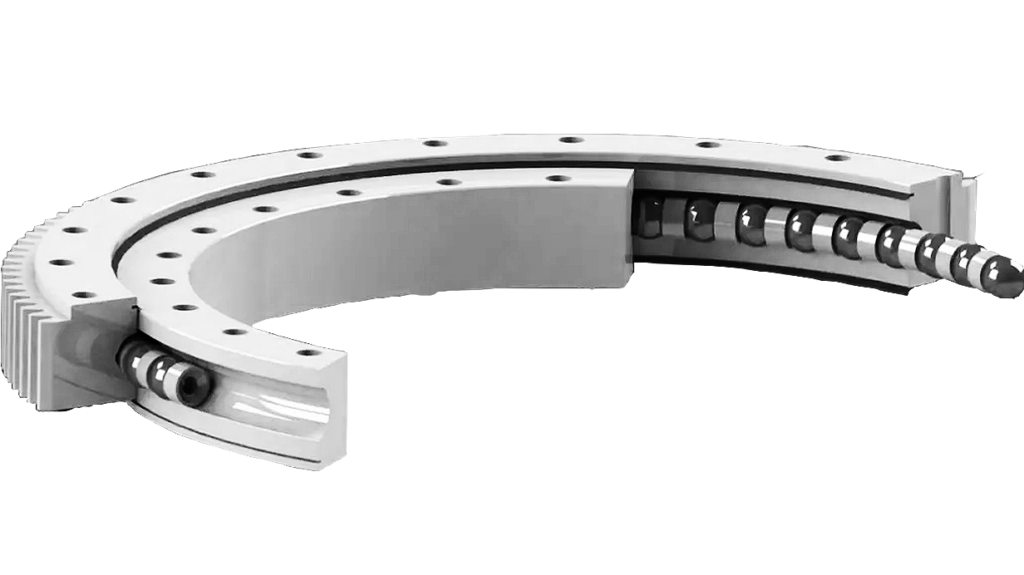
Dimensions 1962.8 × 2376 × 124 mm define the physical envelope for the KUD02200-050VJ15-900-000. The inner diameter of 1962.8 mm establishes the bore interface for mating shafts or structural columns, while the outer diameter of 2376 mm dictates the mounting footprint required on the stationary housing or tower structure. With a cross-section width of only 124 mm, this unit achieves a high load-to-weight ratio, utilizing a four-point contact ball configuration to manage simultaneous axial, radial, and moment loads within a compact profile.
The basic dynamic load rating radial of 1258000 N indicates the rolling fatigue limit under standard operating conditions. Engineers designing for continuous rotation should ensure calculated equivalent loads remain well below this threshold to achieve target L10 life metrics. For static applications or shock loading scenarios, the basic static load rating radial of 15936000 N provides the yield resistance benchmark. Exceeding this static limit risks brinelling of the raceway surfaces, which would introduce vibration and premature failure. Understanding these numeric boundaries allows for precise safety factor calculation during the mechanical design phase.
Specification Reference and Handling Protocols
Before initiating any installation procedure, verify that the delivered component matches the engineering order. Deviations in part numbering can lead to catastrophic incompatibility, particularly with internal gear variants where tooth engagement is critical. Consult the bearing number reference to decode suffix designations related to seals, materials, or manufacturing tolerances.
| Specification Parameter | Value |
|---|---|
| Model Number | KUD02200-050VJ15-900-000 |
| Inner Diameter | 1962.8 mm |
| Outer Diameter | 2376 mm |
| Cross Section Width | 124 mm |
| Type | Four point contact ball slewing bearings (Internal gear type) |
| Basic Dynamic Radial Load Rating | 1258000 N |
| Basic Static Radial Load Rating | 15936000 N |
| Weight | 1013 kg |
Handling requires specialized rigging due to the 1013 kg mass. Lift points must engage the outer ring or designated lugs to prevent deformation. Never roll the bearing on its raceways or apply force directly to the balls. Cleanliness standards during unpacking must exceed ISO Class 5 requirements to prevent abrasive contamination of the hardened steel surfaces. Store the component in its original packaging until deployment, maintaining relative humidity below 60% to inhibit corrosion.
Installation Sequence for Internal Gear Geometry
The internal gear designation requires careful attention to the inner ring tooth interface. Torque transmission occurs through the spline teeth rather than friction locks alone, necessitating precise concentricity between the drive element and the bearing inner race. Improper alignment generates bending moments on the teeth, leading to tooth root fatigue and spalling adjacent to the gear profile.
Prepare all mounting surfaces prior to placement. The mating faces of the inner and outer rings must meet flatness tolerances typically stricter than ±0.05 mm over the contact area. Any dirt inclusion acts as a spacing wedge, distorting the ring geometry and unloading the optimal ball-raceway contact angles. Machine the mounting seats with appropriate surface finish to support the hydrodynamic film in lubricated joints while providing sufficient roughness for secure clamping.
Execute the mounting process using the following protocols:
- Clean all mating surfaces with solvent-free lint-free wipes and inspect for burrs or tool marks that could compromise surface conformity.
- Lift the bearing into position using a crane equipped with a spreader bar to distribute lifting forces evenly across the circumference; avoid localized stress concentrations.
- Align the inner ring teeth with the mating splines gently, ensuring no interference exists before applying axial pressure; hydraulic jacks or heating induction methods may assist assembly if dimensional interference is specified by the design.
- Torque mounting bolts to the manufacturer-specified value using a calibrated wrench in a star-pattern sequence to compress the contact interface uniformly.
- Verify rotational smoothness after installation; manual turning should require consistent torque with no dead zones or binding sensations.
Refer to the Four point contact ball slewing bearings (Internal gear type) category for supplementary technical drawings and cross-sectional diagrams relevant to similar configurations.
Lubrication Strategy and Seal Integrity
Lubrication management is the primary determinant of service life for the KUD02200-050VJ15-900-000. Select a grease compatible with extreme pressure (EP) additives to protect the hardened raceways under the high Hertzian contact stresses inherent to four-point contact designs. Lithium-complex or polyurea base greases generally offer superior oxidative stability and water resistance for industrial environments. Fill volumes should adhere to 30-40% of the free space within the bearing cavity during initial installation; over-greasing induces churning losses and thermal runaway.
Seal performance relies on the integrity of the contact lips indicated by the VJ15 suffix designation. Inspect seals for cuts or abrasions before every operation cycle. Contaminants such as silica dust, weld spatter, or acidic mist can degrade seal materials and allow particulate ingress. If the application involves reverse osmosis or chemical exposure, validate material compatibility of the seal elastomer against the fluid spectrum.
Regreasing intervals depend heavily on speed ratios, temperature rise, and contamination levels. Monitor bearing temperature continuously; a steady-state increase of more than 10°C above ambient signals potential lubrication breakdown or excessive preload. When regreasing, purge old lubricant until clean grease emerges from the drainage channels, then replenish with the recommended volume. Document all lubrication events to track consumption trends that may indicate seal wear or filtration issues.
Preload Calibration and Preventive Maintenance
Four point contact ball slewing bearings often utilize fixed preload determined during manufacture to eliminate internal clearance and maximize stiffness. Preload adjustments via external shims are rarely applicable to this class of sealed unit. During installation, focus on achieving geometric alignment rather than preload modification. Misalignment exceeding the allowable tilt angle reduces the effective contact area, shifting load concentration to fewer balls and accelerating pitting.
Implement a preventive maintenance schedule centered on vibration analysis and visual inspection. Establish baseline vibration spectra during commissioning to detect frequency shifts associated with ball pass frequency outer race (BPFO) or inner race (BPFI) defects early. Schedule periodic audits of mounting bolt tension, as thermal cycling and dynamic loads can cause relaxation over time. Re-torque fasteners to specification whenever deviations exceed 5% of the initial setting.
Assess internal condition through noise and torque variation monitoring. An audible increase in whine or a spike in starting torque often correlates with surface degradation or lubricant starvation. Address these anomalies immediately to prevent cascading damage. Record operational hours and environmental conditions to refine predictive maintenance windows. For engineering support regarding the KUD02200-050VJ15-900-000 or custom solutions, contact FIJ Bearing to request a quote.